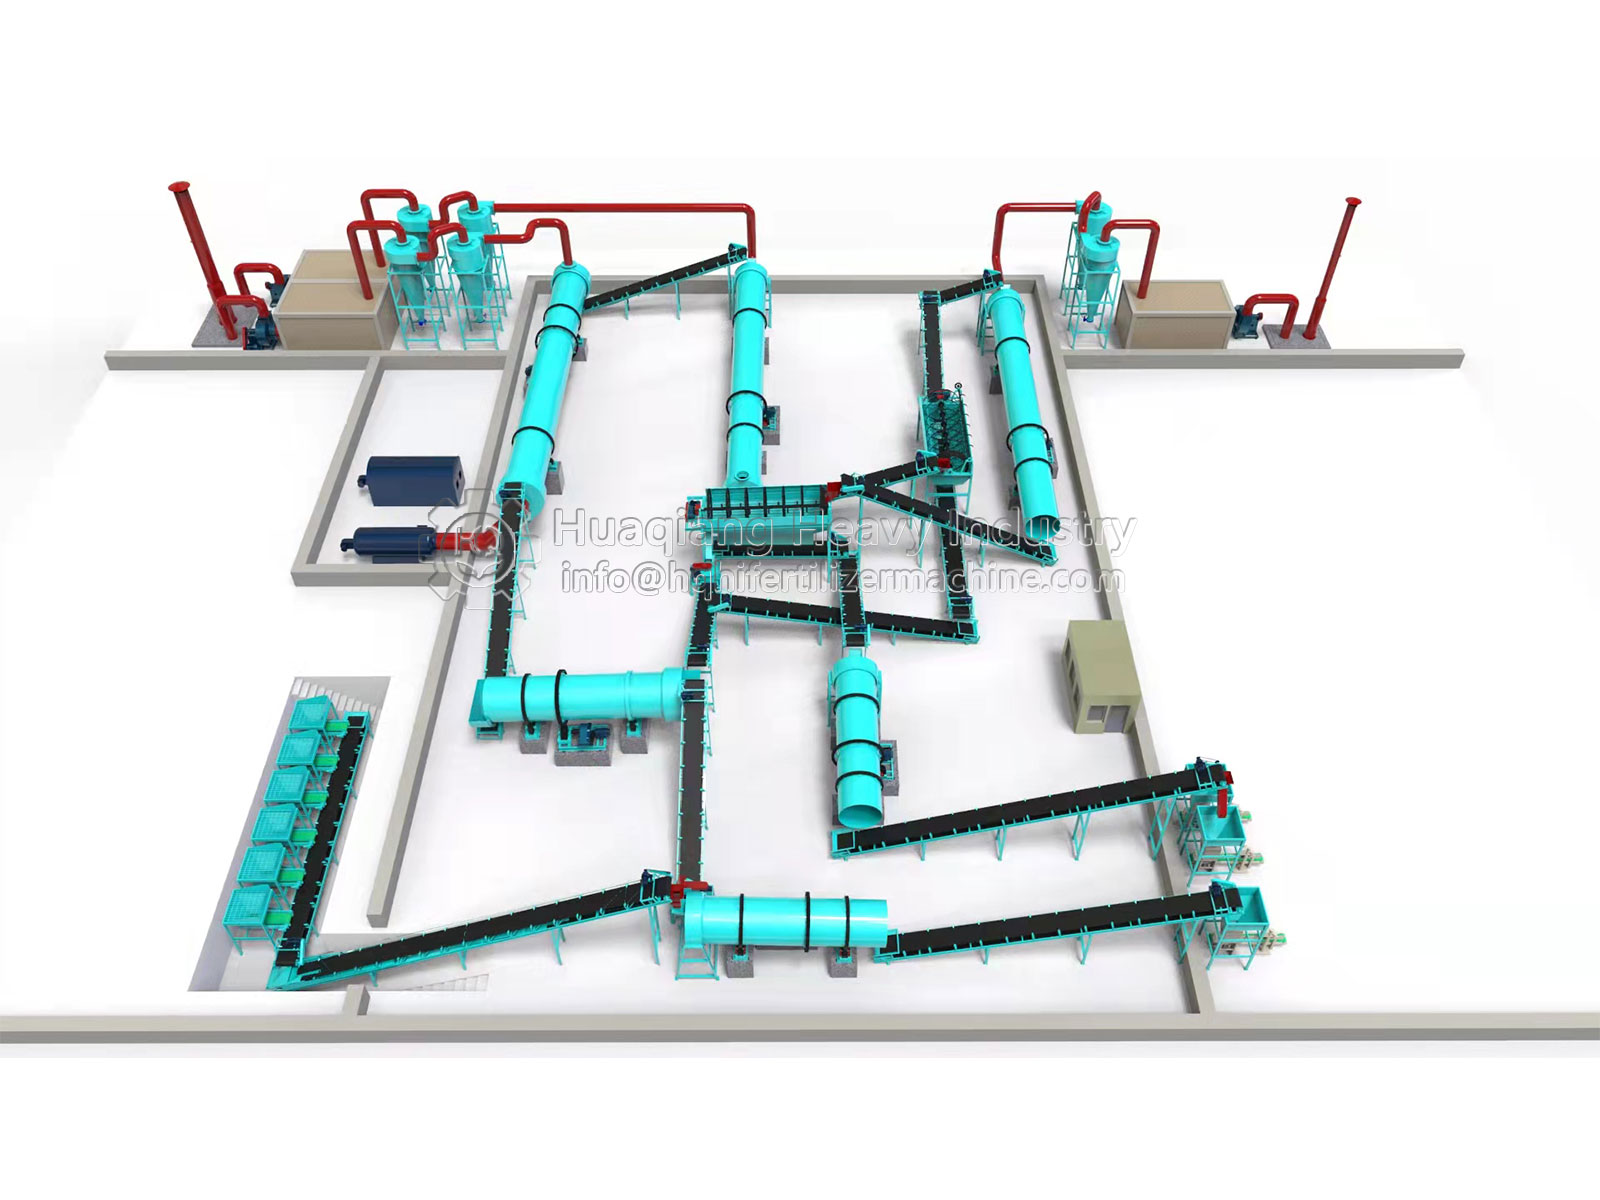
The capacity bottlenecks in organic fertilizer production lines and NPK fertilizer production lines mostly lie not in the rotary drum granulator itself, but in the two “invisible design variables” of the return material ratio and moisture balance. The industry benchmark for the return material ratio in rotary drum granulation is 0.8:1–1.2:1, while for roller-pressed fertilizer granules compaction it’s only 0.3:1–0.5:1. For every 0.1 reduction in the return material ratio, the overall energy consumption of the line can decrease by approximately 5%–8%. After organic fertilizer granulation, the granule moisture content is typically 18%–30%, and it must be dried to below 15%. However, if the moisture content of the feed material for screening is higher than 3%, the screening efficiency will plummet from 95% to below 70%. The critical point for urea granulation is cooling; the discharge temperature needs to be reduced to below approximately 43℃, otherwise the risk of agglomeration increases sharply.
I. Recycled Material Ratio: The True “Design Watershed” Between Rotary Drum Granulation and Roller Compaction Lines
The recycled material ratio is the “quality gate” connecting granulation and finished product. It is defined as the ratio of the amount of material (fine powder + large particles) returned to the system for regranulation to the amount of qualified finished product. It is more critical than the granulator model because the recycled material amount directly determines the design load of each stage of screening, lifting, and drying. Once these loads are fixed in the equipment selection, they are difficult to eliminate later by “adjusting parameters.”
Industry benchmarks clearly show a difference in magnitude between the two routes: the recycled material ratio for rotary drum granulation is generally 0.8:1–1.2:1, while for roller compaction it is only 0.3:1–0.5:1. This does not mean that roller compaction is “more advanced,” but rather that the two forming mechanisms have different inherent tolerances for first-pass yield—rotary drum granulation relies on rolling to grow particles layer by layer, resulting in a wider particle size distribution and more oversize and undersize material; roller compaction relies on pressure to form particles in one pass, resulting in a relatively concentrated particle size distribution after flake crushing.
This difference means the following for NPK fertilizer production lines and organic fertilizer production lines: If the screening machine and elevator are selected based on the return ratio of the roller press, the actual return volume of the rotary drum granulator will quickly consume the design margin. The screening capacity of the rotary drum granulator should be selected based on 1.1 times the granulation capacity, not the finished product capacity. When the return ratio is too high, the first thing to check is not the granulator, but the screening efficiency and screen condition; the capacity and energy savings released by reducing the return ratio from 1.2 to 0.8 are usually greater than replacing it with a larger granulator.
II. Moisture Steps in Organic Fertilizer Production Lines: Granulation Window, Drying Endpoint, and Screening Upper Limit are Three Different Numbers
The most common design error in organic fertilizer lines is managing “granulation moisture” and “screening moisture” as the same target value. In reality, from the discharge of the rotary drum granulator to the finished product packaging, the moisture content decreases in three steps, each step’s target determined by different process constraints.
First Step: 18%–30% after granulation The moisture content of granules after rotary drum granulation typically falls within this range, and the granule strength is not yet fully stable, necessitating a drying process. The upper limit of moisture content is constrained by the granulation process itself—higher moisture content will cause granules to stick together and collapse within the drum; the lower limit is constrained by balling ability—too low moisture content will prevent the powder from forming balls.
Second Stage: Below 15% after drying, 10%-12% for high-standard products. The rotary dryer reduces the moisture content from 18%-30% after granulation to below 15%. Drying temperature is typically controlled between 80-180℃, but organic fertilizers contain organic matter and functional microorganisms, making prolonged high-temperature drying unsuitable; the hot air temperature needs to be matched to the material’s heat sensitivity.
Third Stage: Below 3% moisture content for screening feed. This is the most easily overlooked stage. When the granule moisture content exceeds 5%, screening efficiency drops from 95% to below 70%; the moisture content of granules entering the screening machine should be controlled below 3%, which can be ensured through the dryer’s outlet temperature. If the drying section only removes the urea when the moisture content is below 15%, insufficient screening efficiency will directly increase the return ratio, causing the energy saved in the drying section to be wasted in the screening and circulation sections.
Design Implication: The moisture control point in an organic fertilizer production line should not only be set at the dryer outlet, but also at the screening machine inlet. The cooling section’s role is not just to lower the temperature—screening without cooling easily leads to increased fine powder and particle adhesion; insufficient cooling will negate the moisture advantage established in the drying section.
III. Cooling Boundaries for Urea Granulation: 43℃ and Biuret are Two Independent Constraints
The fundamental difference between urea granulation and the previous two routes is that its design variables include not only “forming” and “moisture content,” but also thermal history. Industrial data from the rotary drum fluidized bed route provides a clear anchor: urea particles are continuously discharged from a bed at approximately 100℃, enter the rotary drum cooler, and are cooled counter-currently to approximately 43℃ with room temperature air, resulting in a product bulk density of 720 kg/m³ and a moisture content of 0.2 wt%. The 43℃ figure is not an arbitrary process preference. Urea is highly hygroscopic; when the discharge temperature is too high, the granules undergo surface slight dissolution and recrystallization during packaging and storage, and crystal bridges rapidly form under the pressure of the feed column. The cooling air temperature should ideally be controlled between 15-25℃, and the discharge temperature should be below 40℃ to avoid moisture absorption and agglomeration. This is logically similar to the organic fertilizer production line’s “cooling to near room temperature before screening,” but urea is more sensitive to temperature deviations because its agglomeration is moisture-driven, rather than driven by microbial activity and fiber rebound like in organic fertilizers.
Biuret is another independent dimension. A key feature of rotary drum fluidized bed granulation technology is that it does not produce biuret during the granulation process. The mechanism is that fine droplets gradually coat the surface of dynamic granules, cooling from the inside out, avoiding prolonged exposure of molten urea to high-temperature zones. 3-5 mm particles have a strength >30 N, and 6-8 mm particles have a strength >80 N. These strength parameters cannot be directly applied to the “balling + drying” route of ordinary drum granulation. If the product is pure urea or a biuret-sensitive formulation, the cooling section design cannot simply calculate the heat exchange area based on “temperature reduction”; the residence time between the melting section and the cooling section must also be included as a boundary condition.
IV. The “Compaction Window” of Fertilizer Granule Compaction: Pressure, Gap, and Rotation Speed Cannot Be Optimized Independently
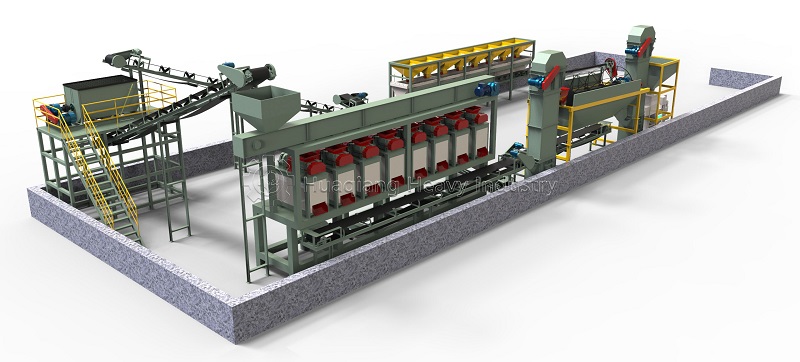
The design logic of roller compaction is completely different from the previous three wet/thermal routes: it does not rely on a water film or molten liquid bridge, but on the combined effect of the pressure applied to the powder by the rollers, the sheet thickness determined by the roller gap, and the pressing time determined by the roller rotation speed.
These three parameters have clear mutual constraints, rather than being independent knobs that can be “optimized” separately: The roller pressure determines the degree of compaction and hardness of the sheet. Insufficient pressure leads to brittle flakes and an increase in fine powder. When encountering excessive fine powder, increasing pressure or feeding speed is the priority, rather than directly reducing speed. The roller speed determines the time the material is compressed in the roller meshing zone. Higher speeds shorten the compression time, reducing the plastic deformation of powder particles and decreasing compaction. However, speed is also a capacity parameter; higher speeds should be preferred to improve efficiency when the process is acceptable. The roller gap determines the flake thickness, which in turn affects the actual pressure distribution experienced by the material within the roller gap.
The design implications for fertilizer granule compaction production lines are: The process cannot proceed in the order of “first determine capacity, then select the roller press, and finally adjust parameters.” Capacity (speed), flake thickness (gap), and compaction quality (pressure) need to be determined as a combination during the selection phase. If the highest rotational speed is selected and then pressure is applied to compensate for the reduced strength after production, it often comes at the cost of increased fine powder circulation and roller wear. Furthermore, the inherent advantage of a low return ratio of 0.3:1–0.5:1 from compaction will be negated.
V. Screening Limitations for Sticky Materials: Why Organic Fertilizer and Urine Base Lines Require “Self-Cleaning” Screening
In all four routes, the return ratio control method shares a common final stage: screening. However, screening itself is selective for materials, and this limitation is more pronounced in the organic fertilizer and urine base line than in NPK.
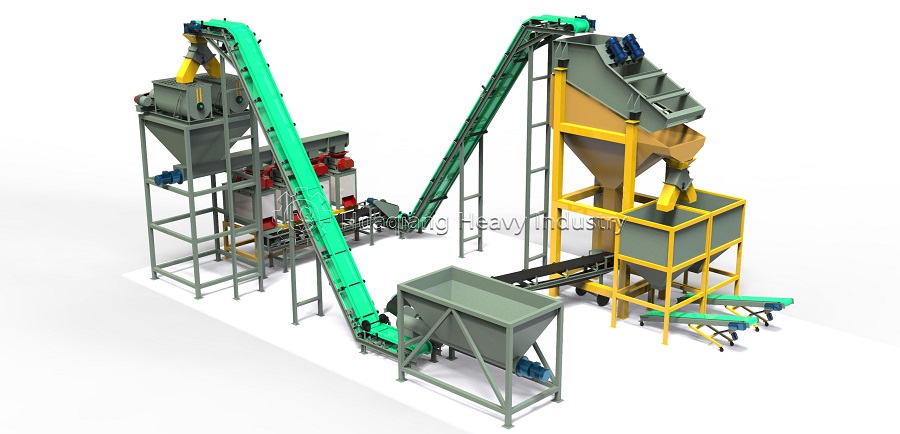
The core advantage of drum screens in the fertilizer industry is their superior anti-clogging ability compared to vibrating screens for wet, sticky materials (3%–8% moisture content): the contact angle between the material and the screen surface changes continuously as the material tumbles inside the drum, giving particles stuck in the screen holes more opportunities to be “thrown out.” However, this advantage is conditional—when processing organic fertilizer or urea-based formulations, it is still recommended to choose a model with a self-cleaning device (external hammer or brush roller), or to use polyurethane screens instead of stainless steel screens, which can improve anti-clogging ability by about 50%.
This limitation applies to organic fertilizer production lines: Even when organic fertilizer granules are dried to below 15%, their surface may still be sticky. The selection of the screening section cannot be based solely on “processing capacity”; the stickiness and self-cleaning ability of the material must be considered as independent selection criteria. For an organic fertilizer line designed with a return ratio of 0.8:1, if the screening machine frequently stops for cleaning due to stickiness and clogging, the actual return ratio will systematically exceed the design value, and both capacity and energy consumption will deviate from expectations.
VI. FAQ: High-Frequency Issues in Production Line Design and Return Control
Q1: The return ratio of the drum line is 1.2:1. To reduce it to 0.8, what should be changed first?
First check the screening efficiency and screen condition, then check the granulation filling rate. The primary cause of a high return material ratio is usually not a low pelletizing rate in the granulator, but rather insufficient screening efficiency, leading to qualified granules being incorrectly fed into the return material. Efficiency drops sharply when the moisture content of the screening feed exceeds 3%-5%. Self-cleaning screens and polyurethane screen surfaces can improve anti-clogging ability by approximately 50%. After screening is normal, the drum filling rate should be controlled at 25%-30% (10%-15% for some operating diameters) to prevent the material bed from sliding rather than rolling.
Q2: The dryer outlet moisture content in the organic fertilizer production line is 12%, so why is screening still clogged?
Check the cooling section and the screening feed temperature; the problem isn’t with continued drying. After drying, the granules are still at a high temperature. If they enter the screening process without sufficient cooling, the granule surface remains soft and easily sticks together, reducing screening efficiency. Cooled granules have higher hardness and a more stable surface, which is beneficial for screening and grading. The target of 3% moisture content in the feed material during screening is the result of the combined effect of temperature and moisture. Simply reducing the moisture content to 12% through drying without controlling the final cooling temperature may still result in substandard screening efficiency.
Q3: Is cooling urea granulation to below 43℃ the same as cooling organic fertilizer to room temperature?
The mechanisms are different, but the design logic is the same. The core constraint for urea cooling is hygroscopic agglomeration—when the discharge temperature is too high, the granules undergo surface micro-dissolution and recrystallization during storage; a cooling air temperature of 15-25℃ and a discharge temperature <40℃ are operational goals to avoid hygroscopic agglomeration. The core constraint for organic fertilizer cooling is granule surface hardness and screening adhesion; screening without cooling will lead to an increase in fine powder. Both use cooling as a means of “decoupling moisture and temperature,” but urea has a lower tolerance for temperature deviations because its agglomeration is driven by hygroscopic factors, rather than the microbial/fiber factors of organic fertilizer.